
Project Overview
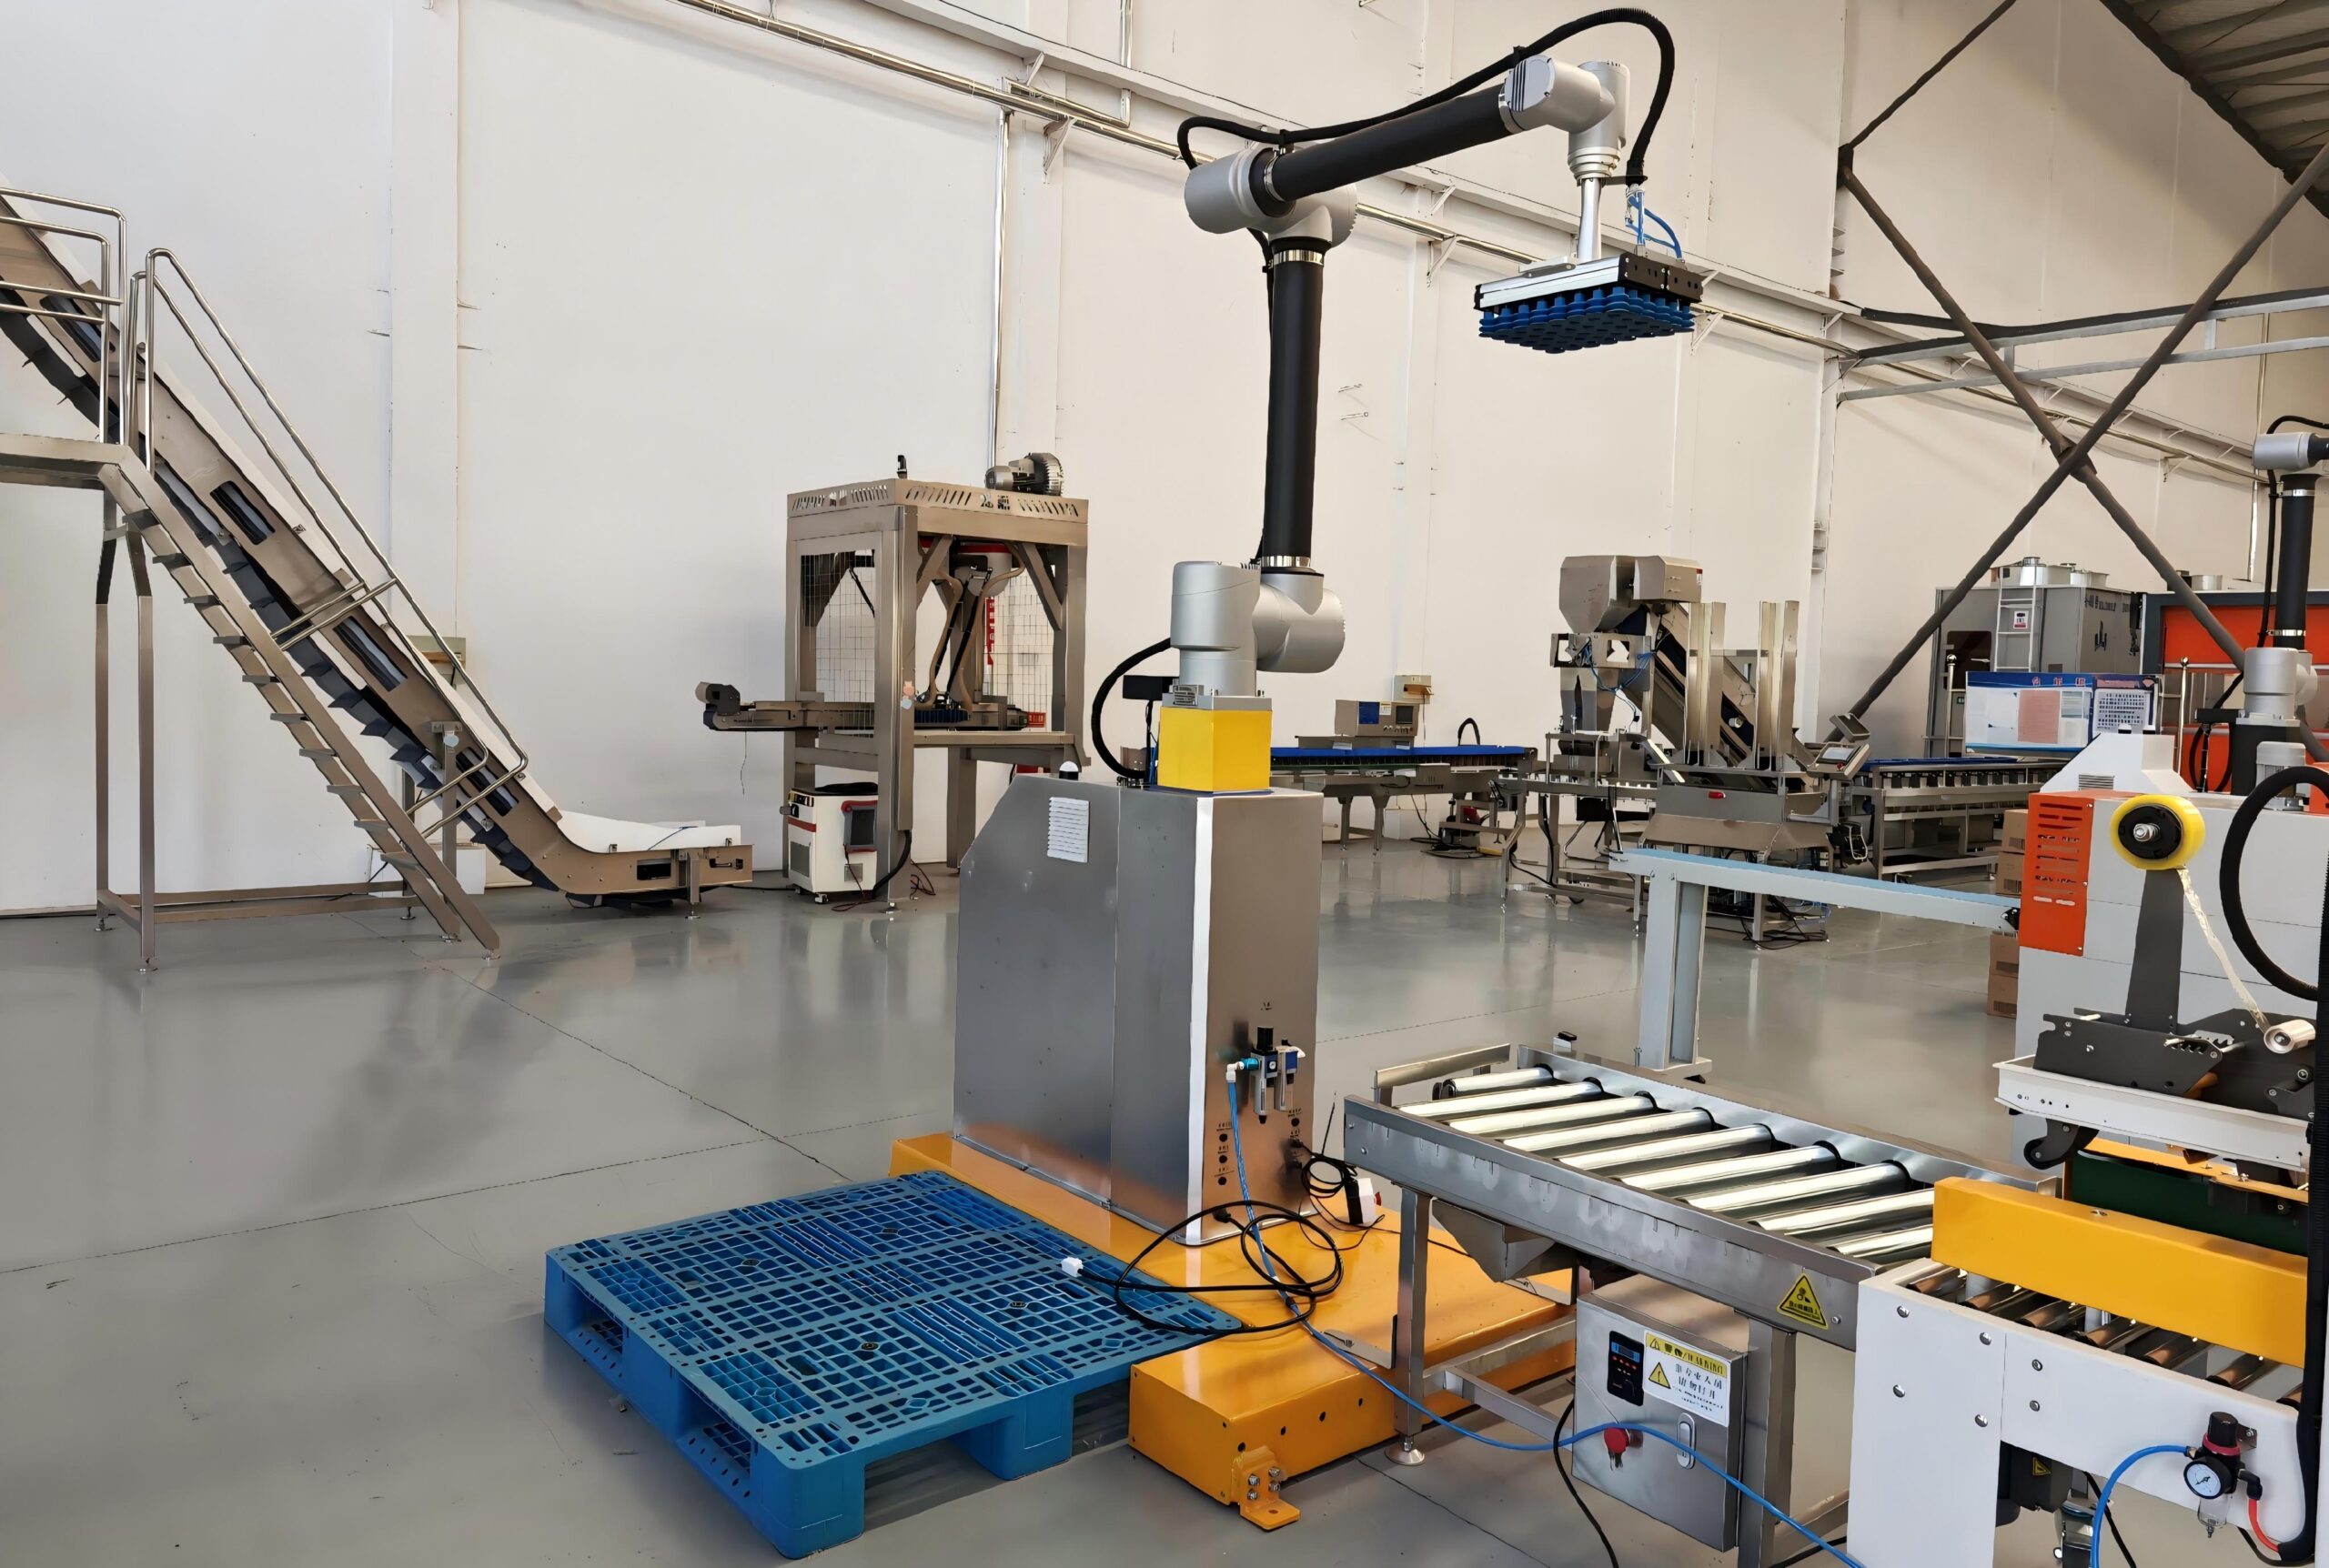
Longreat engineered and deployed a complete robotic palletizing system and custom packaging conveyor line for a high-capacity food processing facility in South Korea. By fully integrating continuous box conveying with precise industrial robotic stacking, this custom automation solution allowed the client to eliminate manual end-of-line bottlenecks, enhance overall factory throughput, and maintain high load stability during long-distance international transit.
Customer Challenge & Operational Background
Prior to implementing Longreat’s custom palletizing automation, the South Korean food processing plant encountered significant end-of-line operational challenges that hindered production scaling:
- High Dependency on Manual Labor: Stacking heavy carton boxes manually required full-time physical labor, resulting in high operating costs, low throughput, and increased worker fatigue.
- End-of-Line Packaging Bottlenecks: Manual box handling and transfer speeds could not keep pace with upstream high-speed filling, sealing, and weight sorting packaging lines.
- Inconsistent Stacking & Pallet Instability: Varied manual stacking quality caused loose or uneven pallet loads, increasing the risk of carton collapse and product damage during shipping and cold storage.
- Integration Needs: The facility required a seamless, continuous box conveying line to connect existing food packaging machines directly with the final palletizing and warehouse staging area.
Our Tailored Automated Solution for Robotic Palletizing System
To address these operational challenges, Longreat customized a high-efficiency end-of-line packaging automation system tailored specifically to food-grade hygiene and performance standards:
1. Automated Box Conveyor & Buffer System
- Continuous Carton Transport: Seamlessly transfers sealed food cartons from the main packaging line straight to the robotic palletizing station without manual intervention.
- Smooth & Stable Handling: Equipped with variable frequency speed drives and precision photoelectric sensors to prevent product collision, box tipping, or carton damage.
- Flexible Space-Saving Layout: Custom-designed modular conveyor layout configured specifically to optimize the customer’s available factory floor space.
2. High-Precision Robotic Palletizing Cell
- Robotic Arm & Custom End-Effector: Utilizes a heavy-duty 4-axis industrial robot fitted with a specialized vacuum/mechanical gripper for secure, high-speed box pickup.
- Multi-Pattern Stacking Software: Features flexible pre-programmed stacking layer patterns suitable for various carton dimensions, weights, and interlock configurations.
- Enhanced Workplace Safety: Enclosed safety fencing compliant with international industrial safety standards (ISO 10218 Industrial Robotics Standard) significantly lowers workplace hazards while maintaining continuous operation.
Technical Specifications & System Configuration
The complete end-of-line packaging and palletizing setup includes the following core machinery and components:
- Core Equipment: Industrial Palletizing Robot, Heavy-Duty Roller & Belt Conveyors, Custom Pneumatic Gripper, Automatic Pallet Dispenser.
- Handling Capacity: Up to 600–800 boxes per hour (depending on box payload and stacking layer pattern).
- Control System: Centralized PLC control panel with intuitive touchscreen HMI for real-time monitoring and easy recipe switching.
- Application: Automated carton conveying, orientation sorting, and palletizing for packaged food cartons and frozen food boxes.
- Target Industry: Food Processing, Frozen Food Packaging, and Industrial Automation.
- Project Location: South Korea.
Measured Results & ROI Impact
Following the installation, testing, and commissioning of the Longreat automation robotic palletizing system, the client achieved immediate operational gains and rapid return on investment:
- 40%+ Increase in Palletizing Efficiency: Stacking cycle speed improved significantly, easily matching the maximum production output of upstream processing lines.
- Labor Reduction & Cost Savings: Reduced manual handling labor at the packaging line end by 2-3 operators per shift, lowering long-term labor expense.
- Improved Transit Stability: Uniform, tightly stacked pallet layers maximized warehouse storage space utilization and eliminated transit damage claims.
- Low Maintenance & High Reliability: Built with industrial-grade components to ensure 24/7 continuous operation with minimal routine maintenance requirements.
Looking for Custom Packaging & Palletizing Automation?
Longreat Automation specializes in robotic palletizing, weight sorting, box conveying, and complete food processing automation lines.
Learn more about our Robotic Palletizer Line or Contact Longreat Automation Experts to get a tailored end-of-line automation proposal for your facility.